


CNC Lathe Machining Service | Precision Turned Parts
Why Buyers Keep This Page Open
| What we do | What it means for your assembly | |
|---|---|---|
| 1 | One-setup multi-operation turning | OD, ID, thread, groove, knurl and cross hole are cut in the same clamping — concentricity does not depend on re-fixturing |
| 2 | Multi-variety mixed batches | Ten different part families can run in one batch; changeover cost stays low for project-based purchasing |
| 3 | ±0.01 mm as standard | Shaft-to-bore fits go together without hand-fitting on the line |
| 4 | Turn + mill combined | Flats, keyways and off-axis holes are cut on the lathe, no second supplier, no extra week |
| 5 | Stainless, brass, aluminium | Prove a design in one material, then switch to the production material |
| 6 | FAI report + material cert | Incoming inspection has a document to check against, and complaints stay traceable |
Every part on this page is turned from bar stock, not carved out of a block — which is why wall thickness, concentricity and thread pitch stay consistent across the batch. Turning, facing, boring, threading, grooving, knurling and cross-drilling happen inside one clamping, so the shoulder face you use as a locating surface is machined in the same setup as the bearing journal it has to align with. That single-setup discipline is the real product here: it is what keeps a ±0.01 mm callout achievable at production volume instead of only on the sample.
What We Turn
| # | Part family | Visible features | Typical use | What we control |
|---|---|---|---|---|
| 1 | Stepped shafts | 3–6 diameter steps, shoulders, relief grooves | Drive shafts, motor shafts, valve spools | Concentricity between steps, shoulder squareness |
| 2 | Knurled grip shafts | Straight or diamond knurl section plus plain shaft | Hand knobs, adjuster rods, press-fit shafts | Knurl OD consistency, knurl-to-shaft transition |
| 3 | Threaded shafts & studs | External thread, undercut, chamfer | Tie rods, adjuster bolts, connecting posts | Thread accuracy, thread-to-shaft concentricity |
| 4 | Flanged bushings | Flange plus thin-wall barrel plus bore | Bearing seats, guide sleeves, seal housings | Wall thickness uniformity, flange face runout |
| 5 | Spacers & standoffs | Through bore, fixed length, chamfered ends | Bearing spacing, PCB standoffs, stack location | Length tolerance, end-face parallelism |
| 6 | Cross-drilled parts | Radial through holes intersecting the bore | Pin connections, oil passages, locking | Hole angle, hole-to-axis intersection |
| 7 | Splined & toothed collars | External teeth, face teeth, bore | Couplings, indexing, locking | Tooth profile, even indexing |
| 8 | Brass fittings | Stepped bore, radial holes, hex or round body | Pneumatic, water and instrument connections | Step depth, sealing-face roughness |
| 9 | Pins & dowels | Small diameter, high length-to-diameter ratio, chamfered ends | Location, hinging, travel limiting | Straightness, diameter tolerance band |
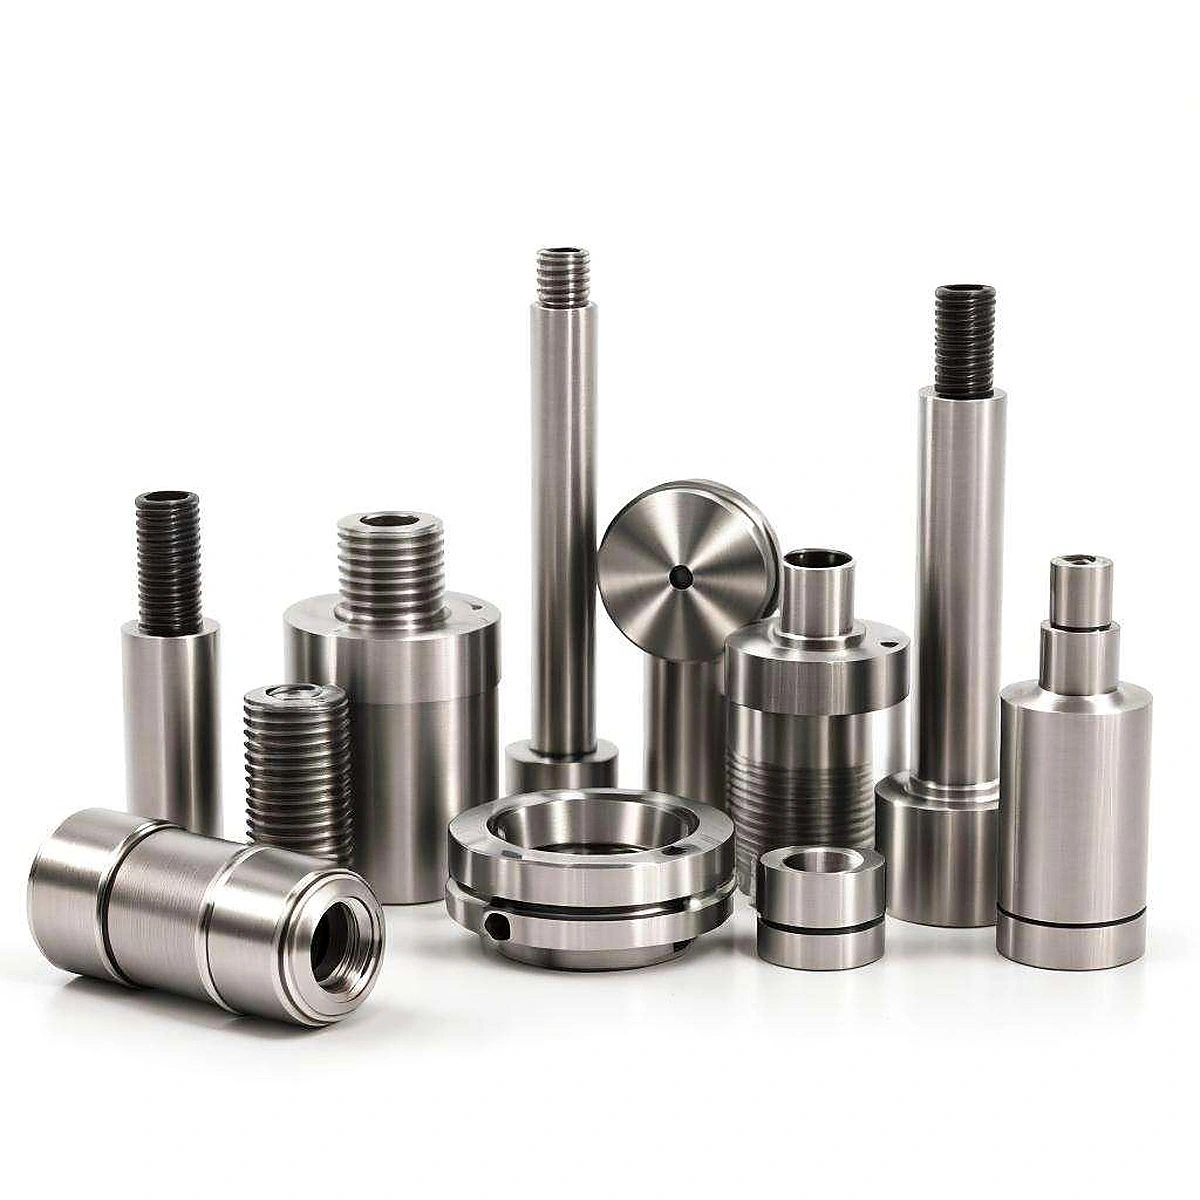
The photo set on this page is deliberately mixed: stainless shafts with diamond knurl, brass bodies with stepped bores and radial holes, flanged sleeves, splined collars and plain spacers all sit in the same batch. That mix is the normal working state of the shop, not a staged photo — which is why multi-variety orders do not carry a heavy changeover surcharge. If your drawing is a turned part with a shoulder, a thread, a knurl, a cross hole or a spline, it belongs on this list.
Capability & Specifications
| Item | Typical range | Tight (on review) | Note |
|---|---|---|---|
| Outer diameter | Ø3 – Ø80 mm | Ø2 – Ø120 mm | Depends on bar stock and workholding |
| Machining length | ≤ 200 mm | ≤ 300 mm | Centre rest required on long parts |
| Linear tolerance | ±0.01 mm | ±0.005 mm | Finish turning or grinding |
| Roundness / concentricity | 0.01 mm | 0.005 mm | Held within one clamping |
| Surface roughness Ra | 1.6 μm | 0.4 μm | Finish turning or subsequent polishing |
| Bore | from Ø1.5 mm | from Ø1.0 mm | Depth-to-diameter > 5 needs step drilling and boring |
| Thread | M1 – M36 / UNC / UNF / BSP | Special profiles to drawing | 100% go/no-go gauge check |
| Knurl | Straight or diamond, module 0.3 – 1.0 | Custom knurl wheels | Referenced to DIN 82 |
| Cross hole | Ø0.8 – Ø10 mm | Multi-angle compound holes | Driven tools |
| Milling on turned parts | Flats, keyways, wrench flats | Multi-face machining | Done on the lathe |
| Batch size | 1 – 100,000 pcs | — | Sample orders from one piece |
| Lead time | Sample 5–7 days / production 15–25 days | Expedite on request | Confirmed against the schedule |
Read this table as a screening tool. If your part falls inside the "Typical" column, a quotation usually comes back within one working day without any back-and-forth. If it needs the "Tight" column, expect one extra round of drawing review, because we will ask which datum actually controls the fit — chasing ±0.005 mm on a dimension that does not affect assembly only adds cost. On cnc precision turned parts, the tolerance that matters is the one that decides whether the part goes into the assembly without hand-fitting.
Materials & Finishing
| Material | Grades | Turning behaviour | Typical use | Finishing available |
|---|---|---|---|---|
| Stainless steel | 303 / 304 / 316L / 17-4PH | 303 free-machining is first choice; 316L corrosion-resistant but gummy | Food equipment, medical, marine | Passivation, electropolishing, nickel plating |
| Brass | H59 / H62 / C36000 | Best machinability, highest as-cut finish | Pneumatic fittings, instrument parts, decorative parts | Polishing, nickel or chrome plating, passivation |
| Aluminium | 6061-T6 / 7075-T6 | Light and fast to cut, thin walls distort | Automation fixtures, heat sinks, visible parts | Anodising (clear or black), bead blasting |
| Carbon / free-cutting steel | 45# / 12L14 / 1215 | High strength at low cost | Structural shafts, connectors | Black oxide, zinc plating, nickel plating |
| Copper / beryllium copper | H62 / C17200 | Good electrical and thermal conduction | Electrodes, contacts, thermal parts | Gold plating, nickel plating, passivation |
For brass turned parts the material choice is almost always C36000 or H62, because free-cutting brass holds a sharp edge and leaves a bright surface straight off the tool — no secondary polishing needed for most fittings. For brass cnc turned parts that will be soldered or brazed, we will ask about lead content before quoting, since leaded brass machines beautifully but is restricted in potable-water and medical applications. Running as a brass turned parts factory that also turns stainless and aluminium, we keep the two material lines on separate machines so brass swarf never contaminates a stainless batch — a small discipline that saves a lot of corrosion complaints later. Stainless 303 is the default for shafts; 316L only when the service environment actually requires it, because it costs more and machines slower.
Inspection & Traceability
| Stage | Method | Output |
|---|---|---|
| Incoming material | Certificate check plus spot spectral analysis | Material certificate |
| First article | Full dimensional measurement (caliper, micrometer, profile projector, CMM) | FAI report |
| In-process | Critical-dimension patrol, tool-life management | Patrol record |
| Final | 100% check on critical dimensions, go/no-go thread gauges | Inspection record |
| Shipping | Sampling plus photo archive, packing to your shipping mark | Pre-shipment report |
On precision turned parts, inspection is where most suppliers quietly lose money and buyers quietly inherit risk. Our rule is simple: whatever dimension the drawing marks as critical gets measured 100% at final inspection, not sampled. Shafts get concentricity checked between the locating shoulder and the bearing journal — the pair that actually decides whether the assembly runs true. First-article reports ship with the sample, so your incoming inspection can compare against a document instead of guessing.
Turn and Mill in One House
A turned shaft that also needs a milled flat, a keyway or an off-axis cross hole is the most common reason a project slips a week. Instead of shipping the part to a second shop for milling, we cut those features in the same program using driven tools on the lathe — which also means the milled flat stays referenced to the turned axis rather than to a re-fixtured surface. That is what our cnc turning and milling services line covers: one drawing, one setup chain, one inspection report.
Applications
| Industry | Typical parts | What matters there |
|---|---|---|
| Industrial automation | Guide shafts, cylinder fittings, fixture posts | Fit accuracy, stable lead time |
| Fluid and pneumatic control | Brass fittings, valve spools, seats | Sealing-face finish, bore concentricity |
| Automotive and new energy | Sensor housings, motor shafts, bushings | Batch consistency, PPAP documents |
| Medical devices | Stainless shafts, connectors, handle parts | Surface cleanliness, material traceability |
| Electronics and instruments | Probe holders, shields, adjuster shafts | Small sizes, no tool marks on visible faces |
| Hardware and consumer goods | Knurled knobs, decorative shafts, connecting posts | Knurl pattern, consistent finishing |
How a Custom Order Runs
| Step | You provide | We deliver | Time |
|---|---|---|---|
| 1 Enquiry | 2D drawing (PDF/DWG) or 3D (STEP/IGES), material, quantity | Process feasibility check | 1 working day |
| 2 DFM review | Confirmation of tolerance, datum, finishing | Cost-reduction suggestions, e.g. relaxing non-critical tolerances | 1–2 working days |
| 3 Quotation | Confirmed batch size and lead time | Formal quotation including tooling notes | 1 working day |
| 4 Sampling | Sample order confirmation | Sample plus FAI report and material certificate | 5–7 days |
| 5 Production | Sample approval | Mass production, final inspection report, packing to shipping mark | 15–25 days |
Custom cnc turning parts move fastest when the drawing arrives complete: material, tolerance class, surface finish, thread standard and the critical dimensions marked. When a drawing is silent on those, we will propose a default and say so in the quotation, rather than quietly choosing something and letting the argument happen at incoming inspection. If the annual volume is real but the first order is small, tell us — tooling and inspection plans can be staged so the first batch stays affordable.
Stock, MOQ and Lead Time
| Item | Detail |
|---|---|
| MOQ | 1 pcs |
| Stock | Semi-finished stock held on standard spacers, standoffs and common pin sizes, quick to modify |
| Sampling | 5–7 working days including FAI report |
| Production | 15–25 working days, depending on finishing and quantity |
| Expedite | Schedule insertion possible, expedite labour charged separately |
| Packing | Your shipping mark; inner packing in anti-static bags, blister trays or oil paper per part |
This is a cnc turning service priced by process route rather than by a catalogue number: the same shaft costs differently depending on whether it needs a ground finish, a knurl or a cross hole. Tell us the annual volume together with the first order quantity and we will quote both, so you can see where the price breaks actually fall instead of assuming they start at a container load. Stock levels move with production — confirm the exact sizes available before ordering.
FAQ
What is CNC lathe machining, and is it the same as CNC turning? CNC lathe machining is turning performed on a computer-controlled lathe: the bar stock rotates while a fixed tool removes material. In everyday use "CNC lathe machining" and "CNC turning" describe the same process. It is the right process for round, symmetrical parts — shafts, bushings, spacers, fittings — and the wrong one for flat plates or deep pockets, which belong to milling.
What tolerance can you actually hold on precision turned parts? ±0.01 mm is our standard production tolerance, and ±0.005 mm is achievable on selected dimensions after drawing review. The honest caveat: on long, slender shafts the limiting factor is deflection, not the machine, so we may recommend a centre rest, a two-pass sequence or a slightly relaxed tolerance on a non-functional diameter instead of quoting a number we cannot repeat across the batch.
Can you run small precision turned parts without a heavy setup charge? Yes, down to Ø2 mm and 1 pc for a sample. Small precision turned parts are usually turned from bar with a guide bush or collet, so the setup is light — but the per-piece inspection cost dominates at low volumes, which is why a 50-piece order is not 50× cheaper per unit than a 5,000-piece one.
Will brass turned parts tarnish, and do they need plating? Bare brass will oxidise and darken over time, faster in humid or sulphur-containing air. For visible brass turned parts we recommend a clear lacquer or nickel plating; for internal fittings where appearance does not matter, bare machined brass is fine and cheaper. Tell us the service environment and we will pick the finish rather than defaulting to the most expensive one.
How do you keep batch consistency across 20,000 pieces? Tool wear is the real enemy, not the first piece. We log tool life, re-measure the critical dimension at fixed intervals, and replace inserts on a count basis rather than waiting for a dimension to drift out. For long runs we also qualify the process on the first article and freeze the parameters, so a different operator on the night shift produces the same part.
What files do you need for a quotation? A 2D PDF or DWG with tolerances and material, plus a STEP/IGES if the part is complex. If you only have a sample, send photos with key dimensions marked and we will quote from that with the assumptions stated. Quotations usually return within one working day.
Request a Quote
Send one drawing — not a catalogue request, an actual part you need made. We will come back with a process route, a tolerance reality check and a price, and if the part should be milled instead of turned, we will say so before you spend money on the wrong process. As a precision turned parts supplier working with both prototype quantities and production runs, the same engineers who quote your job are the ones who set it up on the floor.